High-density, thermal-shock resistant ceramic solutions developed specifically for commercial hospitality, fine dining, and private label retail deployment in Costa Rica.
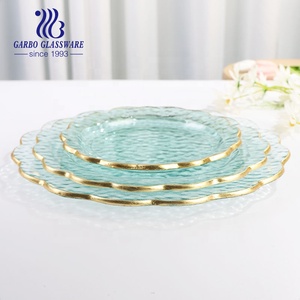
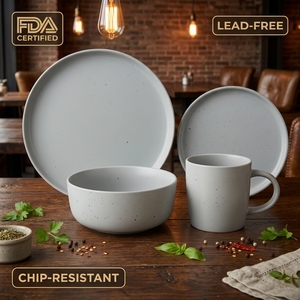
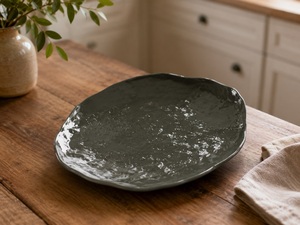
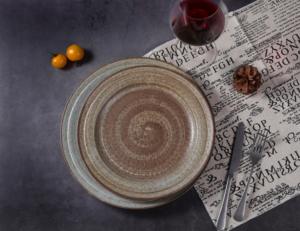
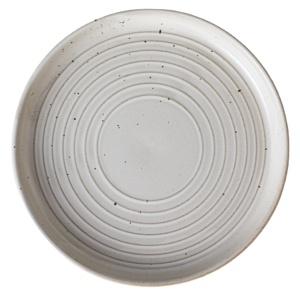
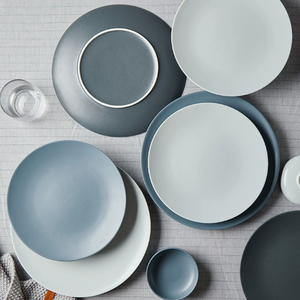
As Costa Rica cements its position as Central America’s premier luxury eco-tourism destination and culinary hub, the demand for high-durability, premium aesthetic ceramic tableware has experienced an unprecedented surge. Sourcing directors, hospitality procurement managers, and commercial distributors across San José, Guanacaste, and Manuel Antonio face unique environmental and operational challenges that traditional earthenware or low-fired ceramics cannot address.
Operating in tropical coastal environments characterized by ambient moisture levels exceeding 85%, severe salt-spray exposure, and intense high-throughput commercial dishwashing requires tableware engineered at the molecular level. High-fired stoneware—vitrified at temperatures between 1250°C and 1300°C—delivers a closed pore matrix with water absorption rates below 0.5%. This technical baseline prevents organic bacterial infiltration, glaze crazing, and structural cracking under thermal shock.
| Material Category | Firing Temp (°C) | Water Absorption (%) | Thermal Shock Resistance | Costa Rica Coastal Suitability |
|---|---|---|---|---|
| Commercial High-Fired Stoneware (OEM/ODM) | 1250°C - 1300°C | < 0.5% (Vitrified) | Superior (ΔT 180°C - 220°C) | Optimal (Zero Mold & Chip Resistant) |
| Standard Earthenware / Terracotta | 1000°C - 1150°C | 5.0% - 12.0% (Porous) | Poor (ΔT < 100°C) | Unsuitable (High Crazing & Humidity Absorb) |
| Low-Fired Soft Porcelain | 1180°C - 1220°C | 1.0% - 3.0% | Moderate | Moderate (Susceptible to Edge Chipping) |
| Vitrified Hotel Porcelain | 1300°C - 1380°C | < 0.1% | High | Good (High Cost, Limited Rustic Textures) |
Combining over three decades of European manufacturing discipline with advanced automated production lines to serve international B2B buyers.
Fired at ultra-high temperatures above 1250°C, our clay body forms a dense crystal structure of needle-like mullite. This eliminates internal air pockets, ensuring total moisture resistance and exceptional mechanical bending strength exceeding 45 MPa.
Our state-of-the-art ceramic laboratory develops proprietary reactive glazes, satin matte textures, and high-gloss vitrified finishes. Every batch is calibrated for glaze-to-body thermal expansion matching, eliminating surface micro-crazing over time.
In-house master mould production guarantees exacting rim profiles, ergonomic handling, and stackability ratios tailored for high-density restaurant service, reducing storage footprint in compact resort kitchens by up to 35%.
Strict quality control protocols govern every stage: from raw clay ball-milling to laser dimensional inspection, pendulum edge-impact testing (ASTM C368 standard), and heavy metal leachability tests complying with US FDA and EU 84/500/EEC norms.
Custom backstamp execution via high-temperature ceramic decal firing or direct bottom-mould engraving. Brands and resort chains can seamlessly embed corporate logos, origin markings, and custom QR codes onto the foot of each vessel.
Utilizing heat-recovery tunnel kilns and recycled clay slurry filtration systems, our manufacturing facility minimizes carbon expenditure per piece, assisting resort groups in maintaining Bandera Azul Ecológica sustainability compliance.
Tailored ceramic properties configured for specific operational environments across the Costa Rican hospitality landscape.
Environmental Factors: Intense ambient humidity, direct ocean sea spray, outdoor alfresco dining exposure.
Operational Demand: Tableware must withstand aggressive salt-air corrosion, prevent glaze degradation under UV light, and maintain structural integrity during open-air wood-fired culinary presentations.
Stoneware Solution: High-density reactive glaze stoneware with sealed foot rims. Zero salt absorption eliminates internal crystallization stress, ensuring long-term surface beauty and zero glaze popping.
Environmental Factors: High table turnover rates, automated high-temperature conveyor dishwashing, tight kitchen staging areas.
Operational Demand: Exceptional mechanical edge-impact resistance, rapid thermal recovery, and stackability design to avoid tipping during fast-paced service.
Stoneware Solution: Matte cement grey and architectural rectangular serving platters featuring reinforced rim profiles and low-profile foot designs that maximize dishwasher rack density.
Environmental Factors: Cooler highland temperatures, high rainfall, farm-to-table oven-to-plate hot dish service.
Operational Demand: Rapid transition capability from high-heat salamanders and ovens (+220°C) to cold mountain air ambient serving conditions without thermal stress fracturing.
Stoneware Solution: Low linear thermal expansion coefficient (COE < 4.5 × 10⁻⁶/K) stoneware formulation designed for direct oven-to-table presentation, holding thermal mass to keep food warm during outdoor rainforest dining.
Environmental Factors: Artisanal seafood dining, tropical citrus marinades (ceviche), heavy natural spice usage.
Operational Demand: Absolute chemical inertness to highly acidic fruit acids and citrus marinades, preventing glaze etching or metallic leaching.
Stoneware Solution: Non-porous, acid-resistant lead-free glazes subjected to rigorous citric and acetic acid immersion tests, providing an pristine canvas for delicate organic plating.
The hospitality sector in Costa Rica is undergoing a transformation driven by three major structural trends:
Luxury resorts are abandoning sterile, uniform white porcelain in favor of warm, organic, hand-tactile stoneware glazes that complement Costa Rica's native natural woods, volcanic stone architecture, and eco-centric design ethos.
Boutique hotel chains and restaurant groups require distinct branding on the reverse side of dinnerware to reinforce brand equity. Our custom backstamping program enables high-precision logo integration under-glaze, preventing wear during heavy dishwashing cycles.
Commercial buyers are calculating annual replacement rates. While low-grade ceramics suffer annual breakages up to 35%, our vitrified stoneware reduces operational replacement rates below 8% per annum, yielding substantial long-term logistics and replacement savings.
Clear technical, logistical, and commercial answers for importers, resort chains, and commercial distributors.
A transparent, technical workflow designed to guarantee design fidelity and zero defect mass delivery.
Submission of dimensional drawings, stackability constraints, volume targets, and glaze finish preferences.
In-house creation of working plaster moulds and laboratory glaze formulation testing to lock thermal shock tolerance.
Physical sample dispatch for customer evaluation, including edge impact, microwave safety, and dishwasher verification.
Automated pressure casting and high-temperature firing at 1280°C with digital pyrometric cone heat curve tracking.
100% visual inspection, sound-ring density resonance checks, and random batch lab verification prior to boxing.
Palletization, container loading supervision, and provision of full documentation for fast customs clearance in Costa Rica.
Partner directly with a certified high-fired stoneware manufacturer. Request custom glaze samples, technical specifications, or an instant OEM production quotation for your hospitality project.