Engineered for high-frequency commercial catering, luxury hospitality, and international retail private labels. Built with low-absorption vitrified stoneware clay bodies and lead-free non-toxic glazes.
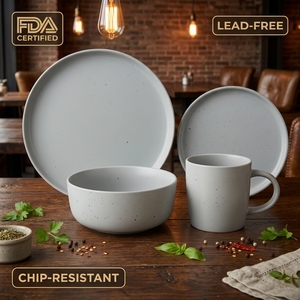
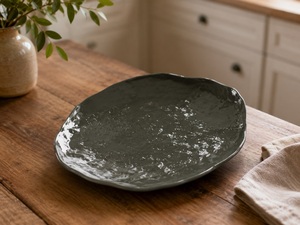
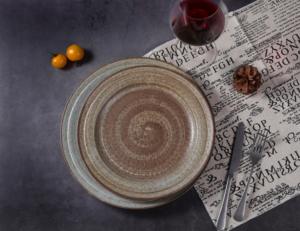
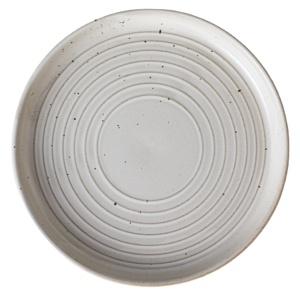
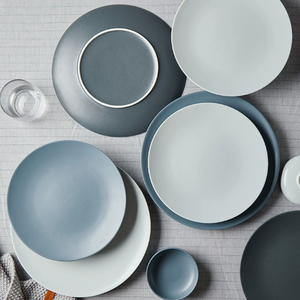
Operating from the historic ceramic hub of Mortágua, Portugal since 1993. Delivering bespoke OEM and private label ceramic stoneware solutions for multi-national retail chains, hospitality groups, and luxury tableware brands.
Our proprietary ceramic laboratory maintains over 1,300 developed glaze recipes, available in high-gloss, satin matt, and artistic reactive finishes. Custom Pantones and physical color standards are matched with thermal stability guaranteed.
Fully compliant with EU Directive 84/500/EEC, Regulation (EC) No 1935/2004, and US FDA requirements. Fired between 1180°C and 1250°C for zero toxic heavy-metal leaching (lead and cadmium free) and ultra-low water porosity (<0.5%).
From custom 3D CAD modeling and master mold production to custom backstamps, laser etching, and eco-friendly e-commerce packaging. We turn bespoke architectural concepts into high-volume production runs.
The global tabletop, kitchenware, and commercial food service supply chains are undergoing a paradigm shift. Enterprise procurement officers, luxury hospitality buyers, and retail category managers are moving away from energy-intensive earthenware and high-carbon porcelain import lines in favor of CE certified sustainable stoneware. Ceramic stoneware—characterized by high-temperature vitrification, high mechanical strength, thermal shock resilience, and zero-porosity performance—presents the optimal balance of functional longevity and environmental compliance.
Executive Insight: Driven by stringent EU ESG regulations, the Carbon Border Adjustment Mechanism (CBAM), and consumer demand for non-toxic dinnerware, European stoneware manufacturing (specifically from Portugal’s ceramic cluster) has emerged as the global benchmark for sustainable, reliable OEM ceramic production.
CE certification in ceramic stoneware manufacturing guarantees that raw materials, glazes, and firing processes strictly comply with European Union health, safety, and environmental protection standards. Procurement teams must navigate specific legal parameters when sourcing international ceramic dinnerware:
Standard ceramic glazes historically utilized lead oxide and cadmium compounds to achieve bright color saturation and smooth gloss finishes. Under EU Directive 84/500/EEC and Regulation (EC) No 1935/2004, strict limits are placed on metal migration into food substances. CE certified sustainable stoneware manufacturers utilize fritted, non-toxic glazes formulations that undergo atomic absorption spectroscopy (AAS) testing. This ensures lead release stays below 0.1 mg/dm² and cadmium below 0.01 mg/dm², satisfying both European CE norms and California Proposition 65 regulations.
The technical definition of stoneware requires a clay body fired to high vitrification temperatures (typically between 1180°C and 1250°C). At these elevated heat profiles, clay particles melt, fuse, and close internal capillary pores. According to ISO 10545-3 testing protocols, certified commercial stoneware must demonstrate a water absorption rate of less than 0.5% (and frequently under 0.1%). Low water absorption prevents liquid absorption, microbial growth, cracking during commercial dishwashing, and glaze crazing over time.
The global ceramic sector is energy-intensive due to thermal kiln requirements. Leading stoneware producers in Mortágua, Portugal have spearheaded sustainable manufacturing solutions that lower Scope 1 and Scope 2 carbon emissions per unit produced:
Modern continuous tunnel kilns utilize heat exchangers that capture waste thermal exhaust from cooling zones and recirculate it directly into raw clay body spray dryers and humidity-controlled drying chambers, reducing natural gas usage by up to 35%.
Unfired scrap clay (greenware) generated during jiggering, casting, and trimming is 100% reclaimed into slurry mix. Post-firing rejected ceramic bodies are crushed into chamotte (grog) and re-incorporated into refractory stoneware formulations, achieving zero clay waste to landfill.
Closed-circuit wastewater treatment facilities utilize physical coagulation and filter-pressing to clarify process water used during glaze spraying and equipment washing. Over 95% of process water is recycled continuously back into clay body compounding.
Corporate procurement strategies are shifting dramatically in response to supply chain vulnerabilities, freight volatility, and ESG mandates. Key strategic trends defining the next half-decade include:
Disruptions in global shipping lanes have driven North American and European brands to re-evaluate far-east procurement. Portugal has solidified its reputation as Europe’s prime stoneware manufacturing powerhouse. Portuguese facilities offer short freight transit times, reliable logistics networks, duty-free trade within the EU internal market, and strict adherence to European labor standards.
Commercial hospitality groups and retail consumers are increasingly rejecting sterile, mass-produced ceramic aesthetics in favor of tactile, organic, and rustic tableware designs. Advanced stoneware manufacturers achieve "artisanal industrialization"—combining high-capacity automated roller kilns with dynamic reactive glaze chemistry. Reactive glazes react organically to slight variations in kiln atmosphere and temperature, ensuring every mass-produced plate possesses a unique visual patina while maintaining structural uniformity for standard stacking.
With modern kitchen spaces prioritizing efficiency, stoneware formulation has evolved to support seamless transition from sub-zero freezer environments directly into 250°C convection ovens, microwave units, and high-speed commercial dishwashers. Thermal shock resistance testing (BS EN 1183) requires stoneware bodies to endure differential temperature spikes exceeding 200°C without micro-fracturing or glaze spalling.
To assist technical procurement buyers in selecting appropriate ceramic bodies for hospitality and retail collections, the following performance matrix compares CE certified sustainable stoneware against alternative ceramic materials:
| Performance Parameter | CE Certified Stoneware | Earthenware / Terracotta | Standard Porcelain |
|---|---|---|---|
| Firing Temperature Range | 1180°C – 1250°C | 900°C – 1050°C | 1280°C – 1400°C |
| Water Absorption (ISO 10545-3) | < 0.5% (Vitrified) | 5.0% – 12.0% (Porous) | < 0.1% (Vitrified) |
| Thermal Shock Resistance | High (ΔT 200°C+) | Low (ΔT < 120°C) | Moderate (ΔT 150°C) |
| Edge Chip Resistance | Superior (High Density) | Poor (Soft Clay Body) | High (Brittle) |
| Glaze Varieties & Texture | 1,300+ Matt, Reactive, Gloss | Limited Gloss Colors | Predominantly White Gloss |
| Commercial Dishwasher Cycle Life | 5,000+ Cycles Compliant | Degrades rapidly | 5,000+ Cycles Compliant |
| Carbon Footprint / Energy Density | Optimized Kiln Profiles | Low Firing / High Scrap | Very High Kiln Energy |
Technical guidance for B2B buyers, private label brand managers, and commercial procurement teams considering custom OEM stoneware manufacturing.
CE Certification confirms that the ceramic stoneware products comply with stringent European Union health, environmental, and consumer safety directives. Specifically for tableware, it verifies that raw materials and finished glazes are certified food-contact safe under EU Directive 84/500/EEC and Regulation (EC) 1935/2004, exhibiting non-detectable levels of heavy metal leaching (lead, cadmium) and maintaining structural integrity under standard commercial usage conditions.
OEM private label manufacturing MOQs depend on shape complexity, glaze formulation, and piece dimensions. Standard production runs typically start at 500 to 1,000 units per item shape for existing glaze libraries, and 2,000+ units for proprietary custom shapes requiring dedicated plaster master molds and specialized glaze R&D. Mixed SKU container shipments are fully supported for complete collection launches.
Stoneware is fired at high temperatures (1180°C–1250°C) until vitrified, offering high mechanical strength, chip resistance, and low porosity (<0.5%). Earthenware is fired at lower temperatures, remaining porous and prone to chipping. While porcelain is also fully vitrified, stoneware offers greater versatility in textured matte and reactive glaze finishes, superior thermal shock resistance for oven-to-table applications, and a warmer, tactile aesthetic favored by contemporary restaurants and boutique hotels.
Yes. Our Mortágua in-house glaze laboratory maintains a library of over 1,300 developed formulas and can engineer custom glaze recipes based on physical color chips, Pantones, or customer-provided sample ceramic pieces. We develop solid gloss, soft satin matt, metallic, and complex multi-layered reactive glazes while conducting rigorous testing to guarantee color stability across mass production firing batches.
All standard Cerages stoneware clay bodies and glazes are technically engineered and laboratory tested for multi-appliance compatibility. They resist thermal shock differentials up to 200°C (392°F), allowing seamless transfer from freezer to oven and microwave. Furthermore, glazes are formulated to withstand high-alkaline commercial dishwasher detergents without scratching, fading, or surface dulling.
Initial 3D CAD design review and technical feasibility assessment takes 3 to 5 business days. Plaster master mold creation and initial physical sample production (including glaze matching) typically requires 2 to 3 weeks. Following customer sample approval and technical backstamp sign-off, full production lead times range between 6 to 8 weeks depending on order volume and kiln scheduling.
Transform your tableware concepts into CE certified, high-performance ceramic stoneware collections. Speak directly with our technical ceramic engineering team in Mortágua, Portugal.